-
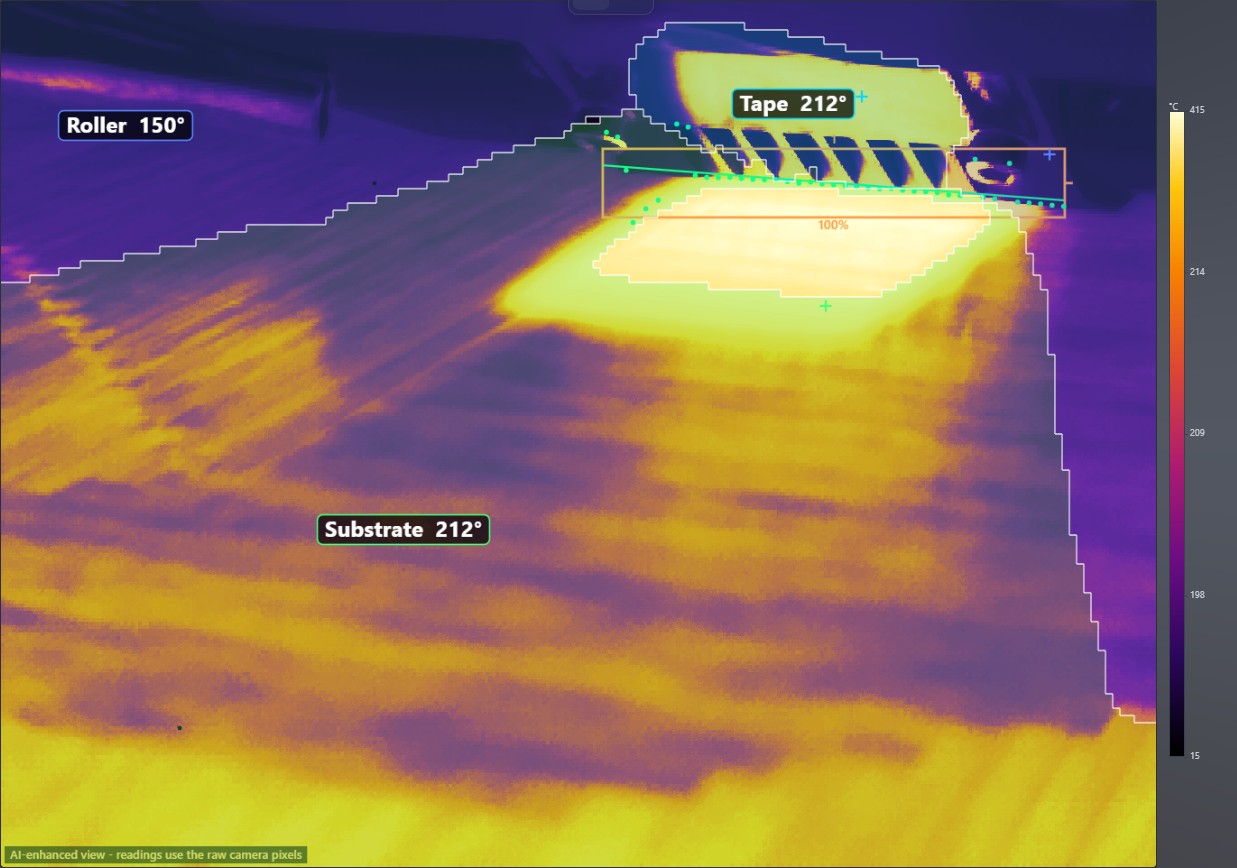
Constant power plus variable speed equals variable heat input. The machine log says the course ran fine; the laminate disagrees.
In automated fiber placement, the heat source delivers constant power — but the placement head does not move at constant speed. That mismatch is one of the most common and least discussed causes of quality variation within a single part.
The governing relationship is simple: faster movement means less exposure time to the heat source. This holds whether the source is a laser, a hot gas torch, an infrared heater or pulsed light.
Head velocity is not constant in practice. It varies during:
With power held constant, each of those regions receives a different energy density at the nip point than the straight, at-speed middle section of the same course.
Changing the exposure time changes both conduction into the substrate and advection along the placement direction. The result is a temperature gradient along the plied layers rather than a uniform thermal history.
Because degree of consolidation and interlaminar bond strength both depend on the temperature reached and the time held there, that thermal gradient becomes a mechanical property gradient. The part is inhomogeneous even though every course was placed exactly as programmed.
Three approaches are common, and they are not equally good:
The power-versus-velocity relationship can be derived rather than tuned by trial. Simulating the optical and thermal behaviour across the velocity range gives the compensation curve directly, before any material is placed — which is considerably cheaper than discovering it through scrapped parts. See real-world simulation and engineering services.
Related reading: Feed rate and velocity, Laser intensity, and Inline monitoring and feedback control.
